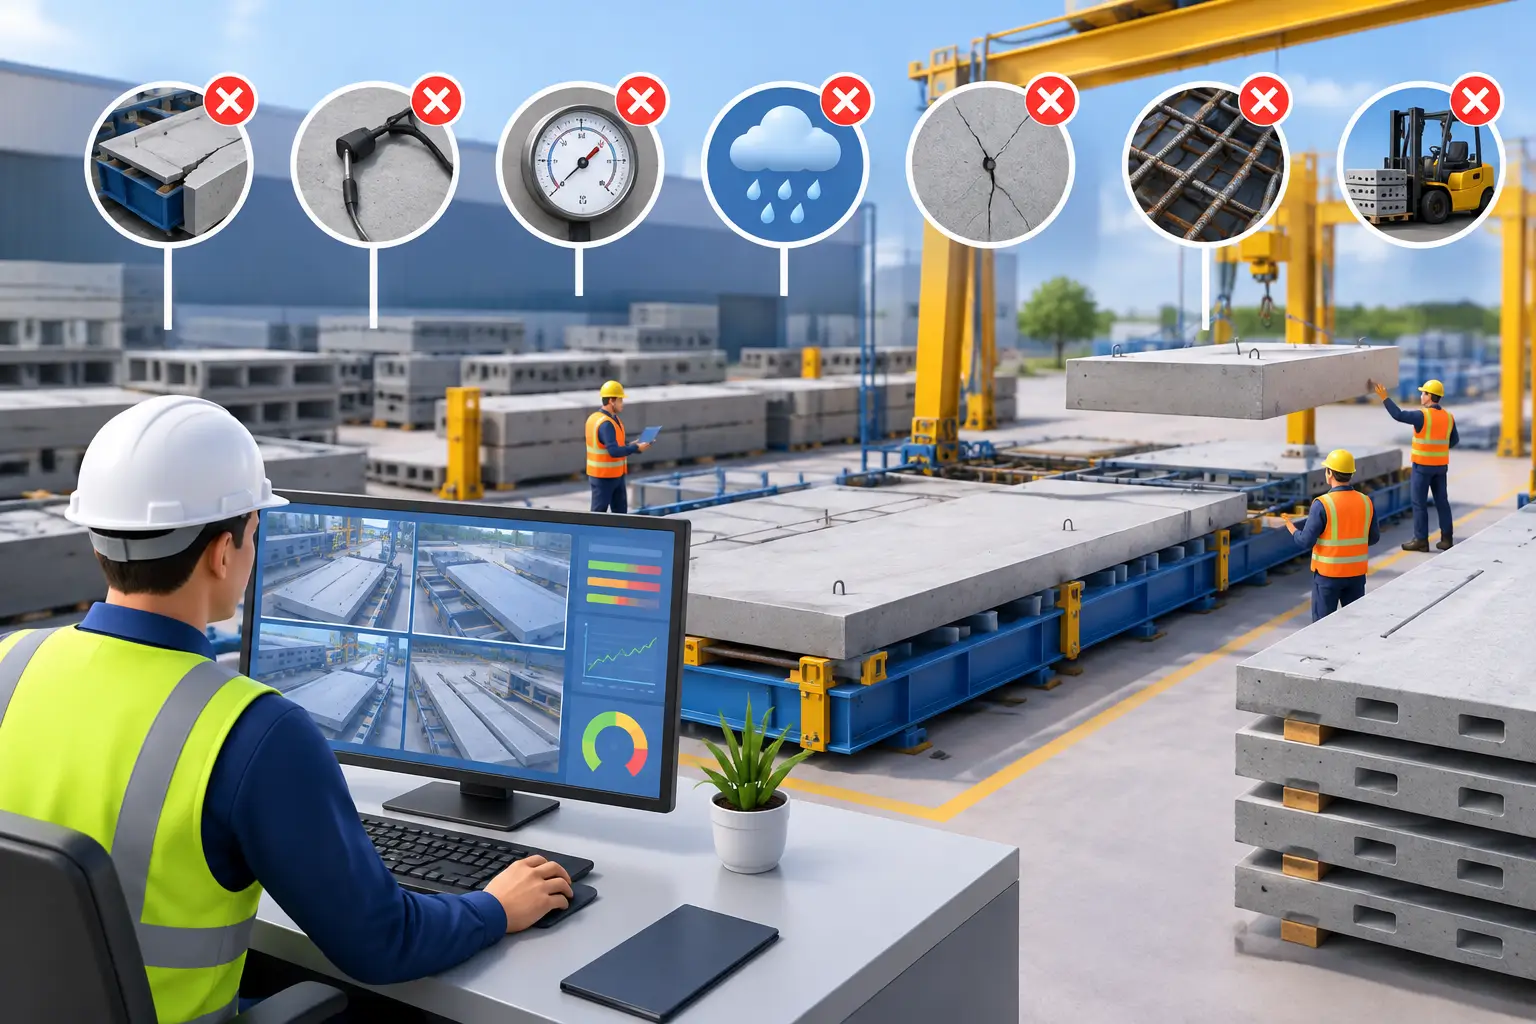
A precast plant can lose a full day of production because a crew waited for a strength result they could have verified hours earlier. More often, the issue is not the concrete mix. It is one of several precast monitoring mistakes that leaves the team without reliable, placement-specific curing and strength data when forms, beds, crews, and trucks are ready to move.
Temperature monitoring and ASTM C1074 maturity testing can give precast producers direct control over stripping, detensioning, lifting, finishing, and curing decisions. But the value depends on how the monitoring program is designed and run. A sensor that is installed in the wrong location, paired with an unrepresentative calibration curve, or checked too late can produce data that is technically available but operationally useless.
The precast monitoring mistakes that affect every cycle
1. Treating ambient conditions as concrete conditions
Plant teams often track enclosure, kiln, or outdoor temperatures and assume those readings explain what the concrete is doing. They do not. Concrete temperature is influenced by cementitious materials, mix temperature, member geometry, insulation, steam exposure, heat loss, and the timing of the curing cycle.
A thin architectural panel and a deep prestressed beam may sit in the same curing area but develop very different internal temperatures. In cold weather, a heater may keep the air within range while the center of a large member retains heat longer than expected. In steam curing, local exposure and cover conditions can create meaningful variation across a bed.
Ambient data still has value for troubleshooting and documenting the curing environment. It should not be the sole basis for strength-release decisions. Embed sensors at locations that represent the critical concrete condition, then use the actual temperature history to calculate maturity and estimate in-place strength.
2. Using one sensor location for every product
There is no universal "right spot" for a sensor. The critical location depends on the product, mix, curing method, structural demand, and decision being made. A location selected for stripping a wall panel may not represent the condition governing detensioning in a prestressed girder.
For larger members, the temperature at the core may differ materially from the surface. For steam-cured products, the section closest to the heat source may not be the slowest or most critical location. A sensor near an edge can also be affected by heat loss that does not reflect the member's interior condition.
Start with the decision the data must support. If the question is whether a member has reached release strength, monitor a location that represents the limiting condition for that release. If thermal history, differential temperature, or durability is also a concern, add locations rather than asking one sensor to answer every question.
3. Applying a maturity curve without validating it for the mix
Maturity is a powerful method, but it is not a generic strength chart. ASTM C1074 requires a strength-maturity relationship developed from the actual concrete mixture being used. Small changes in cement type, supplementary cementitious materials, admixtures, aggregate moisture, water-cementitious ratio, or accelerator dosage can affect strength development.
A curve developed for a summer mix should not automatically be used for a winter mix with a different accelerator package. The same caution applies when a plant substitutes materials, adjusts mix proportions, or transitions to a new source. The concrete may look similar in the field while gaining strength at a different rate.
This is where disciplined QA pays back quickly. Maintain current calibration records for each applicable mix design, identify them clearly in the monitoring platform, and define who approves a curve for production use. If a mix changes, determine whether the existing relationship remains valid before relying on it for critical release decisions.
4. Installing sensors after the critical history has started
Maturity calculations depend on a continuous temperature history from the selected starting point. If monitoring begins after placement, after steam has already started, or after the concrete has entered its rapid temperature-rise period, the missing data can compromise the result.
This mistake often happens during a busy pour sequence. The crew places concrete, finishes the member, and plans to install or activate monitoring equipment later. By then, the first hours of hydration may already be gone. Reconstructing that history from an air-temperature reading or a nearby member is an assumption, not a measurement.
Build sensor installation into the production sequence. Confirm the assigned mix, sensor ID, member or bed location, and start time before placement begins. Rugged embedded sensors are especially useful when the goal is to capture the complete thermal record without exposed wire leads becoming another jobsite or plant-floor failure point.
5. Setting release thresholds without aligning the whole team
A maturity system can report an estimated strength at any time. That does not mean every reported strength is an authorized action point. Release criteria must be tied to approved engineering requirements, plant procedures, and the specific operation being performed.
Stripping strength, lifting strength, detensioning strength, shipping strength, and design strength are not interchangeable. A member may be ready to strip but not ready to handle with a particular lifting configuration. Prestressed work adds another layer of control because detensioning decisions can carry major safety and quality consequences.
The practical fix is simple: configure clear thresholds and name them for the action they support. Then make sure production, QA, engineering, and supervision interpret them the same way. Automated alerts are most useful when they tell the responsible person that a defined decision point has been reached, not when they create another stream of unexplained notifications.
6. Relying on cylinders alone for fast production decisions
Cylinders remain part of many quality programs and may be required by specifications or owner procedures. They provide valuable verification data. The problem begins when teams expect cylinders to represent the exact curing history of every precast member.
Field-cured cylinders can be handled, stored, or cured differently than production members. Lab-cured cylinders are even less representative of in-place conditions. A break result can also arrive after the operational window has passed, leaving forms occupied and crews waiting.
The better approach is not an either-or choice. Use a validated maturity relationship and embedded temperature history for timely, in-place strength decisions. Use cylinders strategically for calibration, verification, acceptance requirements, and quality control. This can reduce unnecessary sampling while improving the relevance of the data used to run the plant.
7. Collecting data but failing to make it usable
Monitoring programs often underperform because the data ends up in handwritten logs, disconnected spreadsheets, or a single employee's phone. When a supervisor needs to know which beds can be stripped before first shift, that information must be visible, current, and easy to defend.
A useful system connects sensor data to the actual workflow: product ID, bed or form location, mix design, placement time, curing event, maturity result, and release threshold. It should also preserve the record needed for an owner, inspector, or internal audit without forcing the QA team to rebuild the story days later.
For high-volume yards, remote visibility matters just as much as measurement accuracy. A cloud-connected platform such as Wake's HardTrack can give production and QA teams live curing data, alerts, and specification-ready reporting from the same monitoring record. That reduces daily checks without reducing control.
Build monitoring around the production decision
The strongest precast monitoring program starts with a simple question: what decision must the plant make, and when? Work backward from stripping, detensioning, lifting, or shipping to define the strength threshold, sensor location, approved maturity curve, reporting requirement, and person responsible for release.
There are trade-offs. A single sensor may be adequate for consistent, smaller products under tightly controlled curing, while complex members or variable curing zones may justify multiple monitoring points. Remote sensors can reduce manual checks, but crews still need clear installation and verification procedures. Technology does not replace plant discipline. It makes disciplined decisions faster and easier to document.
When the schedule is tight, the goal is not more temperature data. It is reliable evidence that the concrete has reached the condition required for the next operation. Get that evidence to the people running the plant before the next production bottleneck arrives.