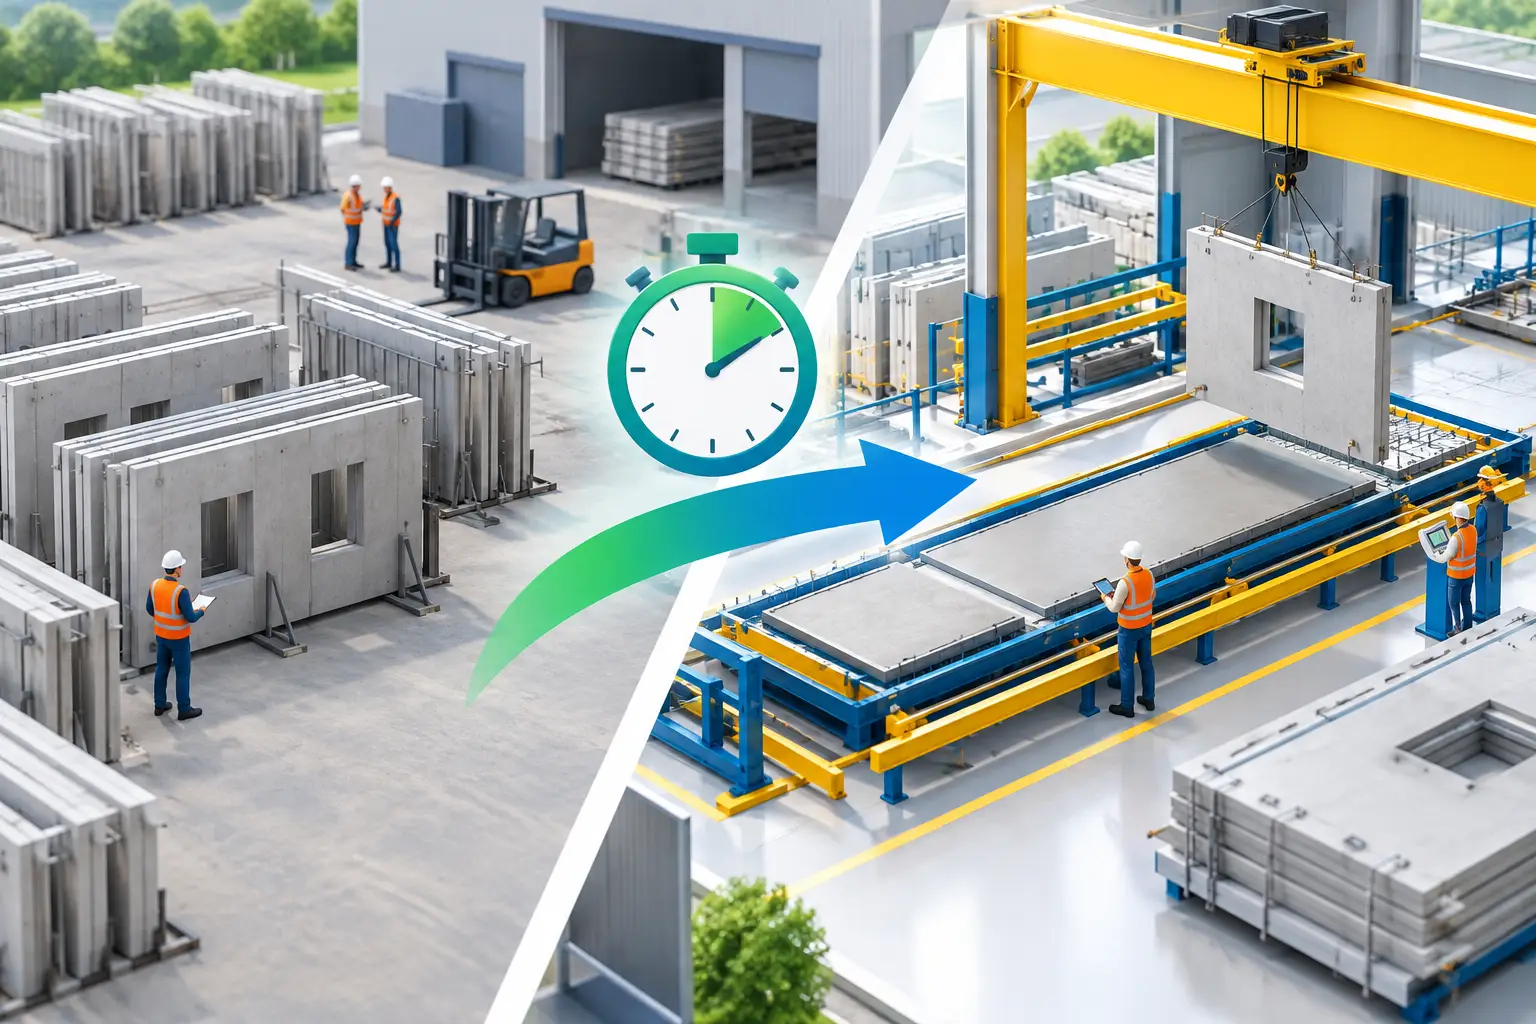
A release delay rarely starts at stripping. It starts hours earlier, when the plant has no defensible answer to a basic question: Has this member reached the strength required to move? In this precast turnaround case study, we examine a representative high-volume plant workflow where temperature monitoring and ASTM C1074 maturity testing replace fixed wait times with real in-place strength information.
This is not about rushing concrete. It is about removing avoidable waiting while keeping release decisions tied to the actual curing conditions inside the product. For producers managing multiple beds, changing mix designs, overnight curing, and tight shipping commitments, that distinction controls both production capacity and risk.
The Precast Turnaround Problem
A precast operation can have capable crews, dependable forms, and a strong mix design yet still lose production time to uncertainty. The typical process is familiar: a member is cast, heat is applied or curing conditions are maintained, cylinders are tested on a schedule, and the bed waits until a result is available or a conservative time threshold has passed.
That approach may work when production volume is low and schedules have room. It becomes expensive when one delayed release holds up form cleanup, reinforcement setup, the next pour, and downstream shipping. A single missed morning release can push work across an entire shift.
The problem is that cylinders do not always represent the member. They are made, handled, stored, and cured under conditions that may differ from the product in the bed. If the cylinders are held in a controlled location while the concrete member sees a different temperature history, the cylinder result can be conservative, misleading, or simply late for the operational decision at hand.
At the same time, producers cannot release a beam, panel, pile, or other member based on a hunch. Release strength is a structural and quality-control decision. The plant needs data that is timely, traceable, and aligned with project specifications.
The Starting Point: A Conservative Release Window
Consider a representative precast plant producing structural members on repeated casting cycles. The operation had a well-established mix and a required release strength. The crew relied on standard curing practices and scheduled testing, but actual turnaround varied with ambient conditions, placement temperature, steam performance, and seasonal changes.
On favorable days, members likely reached release strength before the scheduled decision point. The plant still waited because no one had verified in-place strength. On cooler days or during less consistent heat cycles, the team faced the opposite risk: treating elapsed time as proof of strength when the concrete had developed more slowly than expected.
The production manager did not need more data for its own sake. The manager needed a dependable release decision early enough to organize labor and keep beds moving. QA needed records that could stand up to internal review, owner requirements, and inspection. The plant needed both groups working from the same information.
The answer was not to eliminate cylinders blindly. It was to establish a maturity program that connected the plant's specific concrete mix to measured strength development, then monitor the actual temperature history of concrete in the member.
Establishing the maturity relationship
ASTM C1074 maturity testing begins with a strength-maturity relationship for the specific concrete mixture. This relationship is developed from trial batches and strength tests under controlled conditions. It allows a maturity index, calculated from the concrete's temperature history, to be correlated with compressive strength.
That calibration work matters. Maturity is not a generic strength chart and should not be transferred casually from one mix to another. Changes in cementitious materials, admixtures, aggregate sources, water-cementitious ratio, or curing method may require the producer to review and update the relationship.
Once the relationship was established, the plant defined its release-strength threshold in the monitoring platform. That changed the operational question from, "How many hours has this piece been curing?" to, "Has this member reached the approved release strength under its actual curing conditions?"
The Monitoring Workflow in the Bed
Before placement, the QC team installed rugged temperature sensors at representative locations within selected members. Placement location was deliberate. The objective was to capture the temperature history that governed strength development in the concrete, not merely the air temperature in the curing enclosure.
For thick, heavily reinforced, or thermally variable products, a single location may not tell the full story. The team considered likely temperature gradients, member geometry, heat application, and areas expected to cure slowest. Monitoring the coolest critical location can provide a conservative basis for release, while additional sensors reveal whether curing conditions are consistent across the bed.
With a wireless system such as Wake's HardTrack platform, temperature readings are delivered to a cloud dashboard rather than trapped in a device that must be retrieved from the member. Plant personnel can review live temperature trends, maturity values, and estimated strength from a computer or phone. Automated alerts can notify the right people when a specified strength threshold is reached.
That visibility changes the morning routine. Instead of opening the day by locating paperwork, checking a curing clock, or waiting for a test result, the production and QA teams can see which members are ready, which are approaching release, and which require more curing time.
What the data showed
The initial monitoring period revealed that the plant's fixed release window was too broad to manage production efficiently. Some members reached the required maturity earlier than the standard wait time, particularly when placement temperatures and curing conditions were favorable. Other members developed strength more slowly when the concrete started cooler or the heat cycle was interrupted.
Neither finding was a reason to lower quality standards. Both were reasons to stop treating time as the only control variable.
For early-strength members, verified maturity data allowed the plant to schedule stripping and bed turnover based on actual strength development. For slower members, the data exposed the issue early enough to adjust curing conditions, reassign crews, or revise the day’s plan before a release delay became a surprise.
The plant also found value in the temperature curve itself. A maturity result may confirm strength, but the curve explains how the concrete got there. Unusually low peak temperatures, a flat period during heating, or a rapid cooling cycle can point to curing-process issues that deserve attention. Over time, these records help a producer tune curing practices and reduce variation between beds.
Results That Matter to Production and QA
The primary gain was control. The plant no longer had to choose between conservative waiting and unsupported early release. It could make release decisions using a documented, mix-specific method tied to the concrete in the member.
The operational effect was more predictable turnover. Crews received earlier notice of likely release times, which improved labor planning and reduced idle time around forms and stripping equipment. The plant could also identify members unlikely to meet the next production milestone and act before they disrupted the entire schedule.
QA gained a cleaner documentation path. A proper maturity record can include the monitored member, sensor identification, temperature history, maturity calculation, applicable strength relationship, and release-threshold result. When generated in a specification-ready report, that record is far easier to retrieve than a scattered collection of handwritten logs, cylinder tickets, and verbal updates.
There is also a practical reduction in unnecessary testing. Maturity monitoring can reduce dependence on large numbers of routine cylinder breaks when used under an approved quality plan. The exact approach depends on project specifications, plant procedures, customer requirements, and the producer's validation program. It does not mean cylinder testing disappears in every situation.
Where a Precast Turnaround Program Can Fail
Technology does not correct a weak process by itself. A maturity program can create false confidence if the strength-maturity relationship is outdated, sensors are installed in unrepresentative locations, or personnel treat estimated strength as a substitute for documented acceptance procedures.
Heat curing also requires judgment. Higher temperatures can accelerate early strength, but excessive temperatures or poorly controlled heating can affect concrete performance and create temperature differentials within a member. The goal is controlled curing, not simply the fastest possible temperature rise.
Plants should also decide who owns each action. QA may own calibration and release criteria. Production may own curing execution and bed scheduling. Both groups need access to the same live information, with clear escalation steps when a member does not track toward its required strength.
Building a More Predictable Release Process
A practical rollout starts with one repeated product line or one high-impact bed. Establish or confirm the ASTM C1074 calibration for the mix, select representative sensor locations, define the required release strength, and compare maturity results with the plant's current testing program. That parallel period gives the team confidence in the workflow before it is used for broader scheduling decisions.
From there, use the records to improve more than release timing. Review temperature profiles by product, shift, season, and curing setup. Look for recurring slowdowns. Confirm that curing equipment is producing the intended result. Build reports that allow QA, operations, and customers to see the same defensible history.
The useful outcome is not a faster strip at any cost. It is a release decision made when the concrete is ready, supported by evidence, and visible early enough for the plant to put the next bed in motion.